Compressor sizing requires two parallel calculations: how much air the system actually needs, and at what pressure it must be delivered. Getting either figure wrong produces a machine that is either undersized and unable to sustain production or oversized and expensive to run. This guide explains the flow-rate terminology that trips up most buyers — CFM, SCFM, Nm³/h and FAD — and walks through a systematic method for calculating preliminary compressor capacity from real demand data.
What Does Air Compressor Sizing Actually Mean?
Compressor sizing is the process of determining the minimum free-air delivery (FAD) and discharge pressure a compressor must reliably produce to meet the actual demand of the connected plant. The result is not a model number — it is a set of engineering requirements that a compressor must be verified to meet under site conditions.
Two primary variables drive every sizing calculation:
- Required airflow — the volume of free air the system demands, typically expressed as a continuous or peak rate
- Required pressure — the minimum gauge pressure that must be maintained at the point of use, accounting for all pressure losses between the compressor and that point
These two figures interact directly: a compressor’s rated capacity is always stated at a specific discharge pressure. If the required operating pressure increases, the effective delivered flow typically decreases. Sizing the compressor for the correct combination of flow and pressure is essential; treating them independently leads to mismatches in the field.
A properly sized compressor should handle the calculated system demand plus a reasonable allowance for leakage, system pressure drop, future expansion and duty-cycle variation. What “reasonable” means depends on the specific application — there is no universal percentage that applies to all plants. The allowance should be justified by actual system data.
For guidance on pressure selection separately from flow sizing, see the Compressor Pressure Guide. For a broader view of the selection process, the air compressor selection guide covers compressor technology choices alongside capacity considerations.
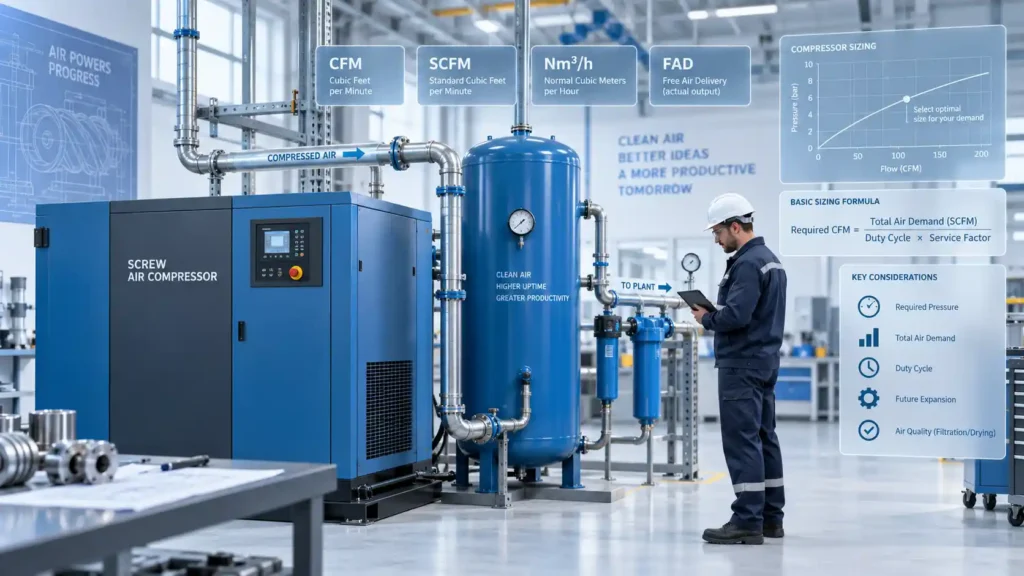
CFM vs SCFM vs Nm³/h vs FAD — What Each Term Actually Means
Compressor flow ratings appear in several different units and on several different reference bases. These are not interchangeable. Using them as if they are produces sizing errors that can exceed 20% in some cases — enough to undersize a machine or purchase unnecessary capacity.
| Term | Reference basis | What it represents | Buyer caution |
|---|---|---|---|
| CFM | Actual inlet conditions (temperature, pressure, humidity at the compressor inlet) | Volume of gas entering the compressor per minute under actual conditions | Changes with altitude and ambient temperature; not directly comparable between sites |
| ACFM | Actual conditions at point of measurement | Same intent as CFM; explicitly labels conditions as “actual” to distinguish from standardized flow | Must state the actual temperature, pressure and humidity to be meaningful |
| SCFM | Standard conditions: 14.696 psia, 60°F, 0% relative humidity (common US basis; verify the standard used) | Flow normalized to a fixed reference state, allowing consistent comparison between machines and sites | The exact reference conditions vary by organization and industry; always confirm what standard is used |
| Nm³/h | Normal conditions: typically 0°C (273.15 K) and 1.01325 bar(a) (ISO standard); some industries use 15°C or 20°C — must be confirmed | Flow normalized to a fixed reference state, SI units | The reference temperature varies — 0°C (ISO), 15°C (gas industry), 20°C (some manufacturers). The multiplier used to convert from SCFM is not a single fixed number |
| FAD | Free Air Delivery: volume of compressed air referred back to the compressor’s stated inlet conditions (ISO 1217 defines this) | The actual delivery of a compressor re-expressed as if the air were at free-air (inlet reference) conditions | Directly reflects compressor performance; compare FAD values only when the stated inlet conditions are the same |
The practical implication is this: when you receive a compressor datasheet quoting capacity in SCFM or Nm³/h, you cannot assume those values are directly comparable without first confirming that the same reference conditions were used. Two compressors rated at “100 SCFM” may have been tested against different standard conditions. Two compressors rated at “170 Nm³/h” may use a reference temperature of 0°C in one case and 15°C in another.
Always request the specific reference conditions alongside the flow figure.
Why Standard Conditions Matter
Gas volume changes with temperature and pressure. A cubic metre of air at 0°C and 1 bar(a) contains more air molecules than a cubic metre at 20°C and the same pressure. If you are comparing compressor ratings, counting molecules — not cubic metres — is what matters for plant performance. Normalized flow figures (SCFM, Nm³/h) exist precisely to make this comparison meaningful by anchoring the volume to a fixed temperature and pressure reference.
The same principle applies to altitude. A plant at 2,000 m elevation has lower ambient pressure than one at sea level. A compressor rated at a given FAD at sea level will deliver less mass of air per minute at altitude because the inlet air is less dense. For installations significantly above sea level, the compressor supplier must be informed so that the capacity can be de-rated and verified against actual site conditions.
This is why FAD — as defined by ISO 1217 — specifies the inlet reference conditions alongside the flow figure. Comparing FAD values without matching inlet conditions is not technically valid.
How to Convert Compressor Flow Units
Two types of conversion are involved and they must not be confused:
Dimensional Conversion (volume per time only)
A dimensional conversion changes the unit of volume and time without adjusting for reference conditions. These are straightforward mathematical conversions:
| From | To | Multiply by | Note |
|---|---|---|---|
| ft³/min (CFM) | m³/min | 0.02832 | Dimensional only — same conditions assumed |
| ft³/min (CFM) | m³/h | 1.699 | Dimensional only — same conditions assumed |
| m³/min | m³/h | 60 | Dimensional only |
| m³/h | ft³/min (CFM) | 0.5886 | Dimensional only — same conditions assumed |
Normalized-Condition Conversion (SCFM to Nm³/h)
When converting SCFM to Nm³/h, the factor 1.699 is often cited. This is valid only when both the SCFM reference and the Nm³/h reference use conditions that produce the same mass-per-volume relationship. In practice, SCFM is commonly referenced to 14.696 psia and 60°F (15.6°C), while Nm³/h is often referenced to 1.01325 bar(a) and 0°C — a 15.6°C difference in temperature.
The correct conversion when reference conditions differ uses the ideal-gas law:
Q₂ = Q₁ × (P₁ / P₂) × (T₂ / T₁)
Where:
Q₁ = flow at reference condition 1 (e.g., SCFM at 14.696 psia, 60°F / 288.7 K)
Q₂ = flow at reference condition 2 (e.g., Nm³/h at 1.01325 bar(a), 0°C / 273.15 K)
P₁, P₂ = absolute pressures of respective reference conditions
T₁, T₂ = absolute temperatures (Kelvin) of respective reference conditions
Note: Pressures must be absolute (psia, bar(a)), not gauge.
Applying this to the common US-to-ISO case:
- Reference 1 (SCFM): 14.696 psia = 1.01325 bar(a); 60°F = 288.7 K
- Reference 2 (Nm³/h at 0°C): 1.01325 bar(a); 0°C = 273.15 K
- Pressure ratio: 1.0 (same absolute pressure)
- Temperature ratio: 273.15 / 288.7 = 0.9461
Result: SCFM × 1.699 × 0.9461 ≈ SCFM × 1.607 to obtain Nm³/h at 0°C reference.
The simple 1.699 multiplier gives m³/h at the same conditions as the SCFM reference — not Nm³/h at 0°C. When in doubt, state the reference conditions for both sides of the conversion and confirm with the manufacturer.
How to Calculate Required Compressor Capacity
The required compressor capacity is not simply the sum of all connected tool nameplates. That figure — connected demand — describes the theoretical maximum if every device ran simultaneously at full load. In most plants, this never occurs.
A more accurate approach builds required capacity from:
List every pneumatic device, tool and process that uses compressed air. Record the rated air consumption and duty cycle (fraction of time it runs at full demand).
Apply a demand factor (duty cycle) to each device. Sum the resulting demands for devices that operate simultaneously. This is the real operating demand, not the connected maximum.
Compressed-air systems leak. The leakage rate depends on system age, maintenance standard and fitting types. It must be estimated or measured and added to process demand. Poorly maintained systems can lose a substantial fraction of total system flow.
Every component between the compressor and the point of use reduces pressure: piping friction, filters, dryers, regulators, valves. The compressor must deliver at a discharge pressure high enough to maintain minimum system pressure after all these losses.
Some processes create short-duration demand spikes above the average. An air receiver can buffer these peaks without requiring the compressor to be sized to the peak transient. Understand the duration and frequency of peaks before adding them to the compressor requirement.
If growth is foreseeable, add an allowance that reflects the planned expansion — not an arbitrary percentage. A second compressor installed later may be a better strategy than over-sizing the initial unit.
The Air Receiver: Buffer, Not Substitute
A correctly sized receiver lets the compressor run at a more stable duty cycle, buffers short demand peaks and provides a reserve during compressor switchover. It does not compensate for a permanently undersized compressor. If the average system demand exceeds compressor delivery, the receiver will drain and system pressure will fall regardless of receiver volume. Size the compressor for the average demand; size the receiver for peak transient management and control stability.
Continuous vs Intermittent Demand
Continuous-demand devices (cooling air, purge flows, process controls) consume air at a relatively fixed rate. Intermittent devices (pneumatic tools, actuators, air-blast guns) draw high peak flows briefly. Each requires different treatment in the demand calculation. Treating all intermittent loads as continuous will consistently oversize the compressor; ignoring peak intermittent loads entirely will cause pressure dips in operation.
Worked Compressor Sizing Example
The following is a hypothetical engineering example using assumed values. It demonstrates method, not actual product performance. All figures must be verified against real plant measurement and manufacturer-rated compressor data.
Scenario
A manufacturing facility has the following hypothetical pneumatic consumers:
| Device | Rated demand (SCFM) | Qty | Duty factor | Effective demand (SCFM) |
|---|---|---|---|---|
| Assembly air tools | 20 | 4 | 0.40 | 32.0 |
| Blow-off nozzles | 12 | 3 | 0.60 | 21.6 |
| Pneumatic cylinder actuators | 8 | 6 | 0.30 | 14.4 |
| Instrument air (continuous) | 10 | 1 | 1.00 | 10.0 |
| Simultaneous process demand | 78.0 SCFM | |||
Step 1 — Add estimated leakage
Assume a well-maintained modern system with leakage estimated at 10% of process demand:
78.0 × 0.10 = 7.8 SCFM
Subtotal: 78.0 + 7.8 = 85.8 SCFM
Step 2 — Determine required discharge pressure
Minimum tool operating pressure: 6.0 bar(g) [87 psi(g)]
Estimated piping and filter pressure drop: 0.5 bar(g) [7.3 psi(g)]
Estimated dryer pressure drop: 0.2 bar(g) [2.9 psi(g)]
Required compressor discharge pressure: 6.0 + 0.5 + 0.2 = 6.7 bar(g) [97 psi(g)]
Select a compressor rated for 7 bar(g) [102 psi(g)] discharge to provide a small working margin above the minimum needed.
Step 3 — Convert to Nm³/h (if needed for European supplier comparison)
Using SCFM at 60°F / 14.696 psia → Nm³/h at 0°C / 1.01325 bar(a):
85.8 SCFM × 1.607 ≈ 137.9 Nm³/h
What this means for compressor selection
The preliminary system requirement is approximately 86 SCFM (138 Nm³/h) at 7 bar(g) discharge. This is the calculated demand figure — not automatically the compressor nameplate rating. The selected compressor must be verified to deliver at least this flow at the rated discharge pressure under site conditions (actual inlet temperature, altitude, cooling water temperature). Compressor FAD data at the operating pressure must be confirmed against manufacturer-rated performance, not just the nameplate.
Pressure, Pressure Drop and Compressor Selection
Discharge pressure selection directly affects energy consumption. Compressor specific power (kW per unit of delivered flow) increases with discharge pressure. Selecting a higher pressure than the process actually requires increases running costs for every hour of operation.
The common reasons for unnecessary pressure selection include:
- Assuming a high safety margin when the actual pressure loss through the system is unknown
- Accommodating the single highest-pressure tool in the plant without considering whether it could be served separately
- Inheriting the pressure from an older system without re-evaluating whether it is still appropriate
Before fixing the discharge pressure, map the pressure drop through every system component — piping, separators, filters, dryers, condensate drains and any downstream control valves. This establishes the actual required compressor discharge pressure from first principles rather than estimation. Reducing operating pressure where possible reduces energy costs. For detail on pressure selection methodology and its efficiency implications, see the Energy Saving Guide.
Pressure Basis in Calculations
When using gas laws or performing normalized-flow calculations, always use absolute pressure — bar(a) or psia. Gauge pressure readings (bar(g), psi(g)) must be converted by adding atmospheric pressure (approximately 1.01325 bar or 14.696 psi at sea level). Mixing gauge and absolute values in equations produces incorrect results.
Common Compressor Sizing Mistakes
Summing all nameplate ratings without duty-cycle adjustment invariably produces an oversized machine with poor part-load efficiency. Measure or estimate actual simultaneous demand.
A system without a documented leakage survey will deliver a larger fraction of total compressor output to atmosphere than to productive use. Leakage must be estimated, measured and included in the demand figure.
Selecting pressure at the compressor outlet without accounting for downstream losses causes insufficient pressure at the point of use — even with a correctly sized flow rating.
Using a fixed conversion without confirming reference conditions introduces error. Always state and match reference conditions when comparing flow ratings from different sources.
A receiver buffers transient peaks. It cannot sustain the system if the compressor cannot meet average demand. Size the compressor for average demand and the receiver for peak management.
A compressor installed at elevation delivers less mass flow than at sea level. Inform the supplier of site elevation so FAD figures can be correctly adjusted.
What Data Should You Send to a Compressor Supplier?
A compressor supplier cannot size a machine from flow and pressure alone. The more complete the information provided, the more accurate the selection and the lower the risk of a mismatch between purchase and performance.
Final Engineering Takeaway
Compressor sizing begins with a demand calculation based on actual simultaneous use — not theoretical connected load. The calculated figure must include leakage, account for system pressure losses, and be expressed in a clearly defined flow unit with a stated reference condition. The resulting flow-and-pressure requirement is then matched against manufacturer-rated FAD data at the operating pressure and site conditions.
No formula produces a final compressor selection directly. The calculation produces a verified requirement that the compressor must then be confirmed to meet. Manufacturer performance data — not nameplate alone — is the final reference.
To size a compressor against your actual application, send the required flow (with reference basis), minimum working pressure, site altitude, ambient temperature range, duty cycle and cooling arrangement. Review the full compressor range and contact the technical team with the checklist above to receive a model recommendation verified against the operating conditions.
Frequently Asked Questions
Is CFM the same as SCFM?
No. CFM describes actual volumetric flow at the real conditions at the measurement point (temperature, pressure, humidity). SCFM normalizes that flow to a fixed reference condition (commonly 14.696 psia and 60°F in North American practice) so that different compressors and sites can be compared on an equal basis. A compressor rated in CFM at inlet conditions and one rated in SCFM cannot be directly compared without knowing the inlet conditions for the CFM figure.
Can I convert SCFM to Nm³/h by multiplying by 1.699?
Only if both SCFM and Nm³/h use the same or equivalent reference conditions. The factor 1.699 is a dimensional conversion from ft³/min to m³/h — it does not adjust for the temperature difference between typical SCFM reference (60°F / 15.6°C) and the ISO Nm³/h reference (0°C). When converting between these specific references, the correct multiplier is approximately 1.607. Always confirm what standard conditions each rating uses before applying a conversion factor.
What is FAD and why does it matter for compressor selection?
FAD (Free Air Delivery) is the volume of compressed air a compressor actually delivers, recalculated to the stated inlet reference conditions (per ISO 1217). It is the most direct measure of what the compressor actually produces in operation, as opposed to the theoretical displacement of the rotors or pistons. When comparing compressors, FAD figures at matching inlet conditions and at the same discharge pressure give the most reliable basis for comparison. FAD values at different discharge pressures or inlet conditions cannot be directly compared.
How much leakage should I allow for in the sizing calculation?
There is no universally correct percentage — leakage depends on the age and condition of the system, the type of fittings and connectors used, and how rigorously it is maintained. A new, well-installed system may leak very little. An older system in poor condition can leak a significant fraction of total compressor output. The correct approach is to measure leakage during a no-demand period (all process equipment shut off), or to commission an air audit before sizing a replacement or additional compressor. Adding an allowance without measurement introduces uncertainty in both directions.
Does a larger air receiver let me use a smaller compressor?
A receiver can reduce the required compressor size only for applications where demand is genuinely intermittent and the compressor has time to recharge the receiver between demand events. If average demand consistently exceeds compressor delivery, no receiver volume will sustain system pressure — the compressor must meet average demand directly. Receivers are correctly used to buffer short-duration peaks, smooth compressor on/off cycling, and provide reserve during maintenance, not to compensate for a systematically undersized machine.
Does site altitude affect compressor capacity?
Yes. At altitude, ambient pressure is lower than at sea level, which means the inlet air contains fewer molecules per cubic metre. A compressor that draws a given volume of air per minute at altitude delivers less mass of air — and therefore less compressed-air mass flow — than the same machine at sea level. For installations above approximately 500 m, site elevation should be explicitly provided to the supplier so that the FAD can be adjusted to reflect actual inlet conditions. The degree of de-rating depends on the specific altitude and compressor design.
Why should I not just add a 20% safety margin to my calculation?
A blanket safety margin is a substitute for understanding the actual sources of uncertainty in the sizing. It may oversize the compressor unnecessarily — increasing capital cost and reducing part-load efficiency — or it may undersize in cases where the real uncertainty exceeds 20%. The correct approach is to quantify each uncertainty separately: leakage (measure it), future expansion (plan it), peak demand (identify it), pressure drop (calculate it). Each of these has a specific engineering basis. An unexplained 20% addition papers over the sizing work rather than resolving it.